Key challenges in industrial detergent and cleaning product packaging
Chemical compatibility and packaging resistance
We work closely with our customers to identify packaging solutions that are fully compatible with their formulations and maintain product stability throughout their lifecycle.
Loss of performance due to chemical permeation
We incorporate barrier technologies that help prevent permeation, ensuring your product retains its efficacy and properties throughout storage and distribution.
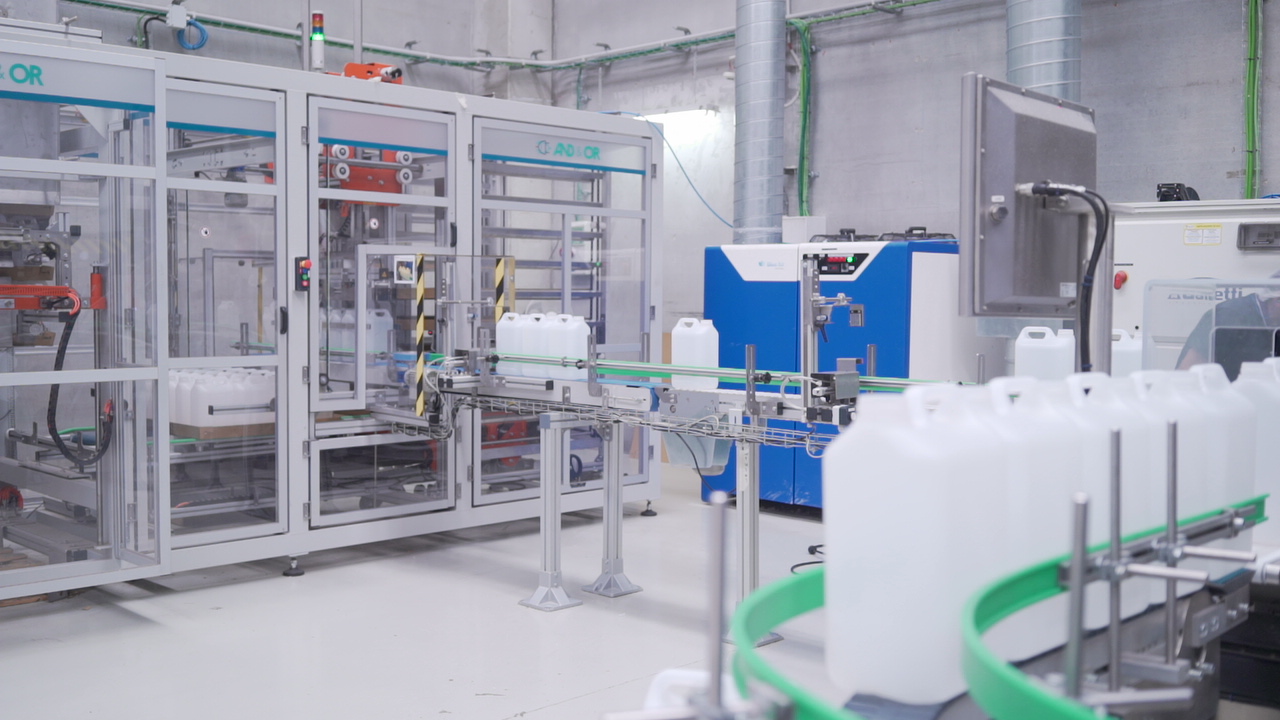
Challenge on automated packaging lines
We design packaging adapted to industrial processes to minimise downtime, rejects, and issues during filling, capping, and labeling.
Regulatory compliance
We manufacture certified packaging that complies with current regulations, providing safety, reliability and peace of mind at every stage of the process.
Sustainability
We optimize material usage and develop recyclable packaging solutions that reduce environmental impact without compromising performance.
Inefficient logistics
Our packaging is designed to optimize storage, stacking, and transport, helping to reduce costs and improve operational efficiency.
Recommended products and formats
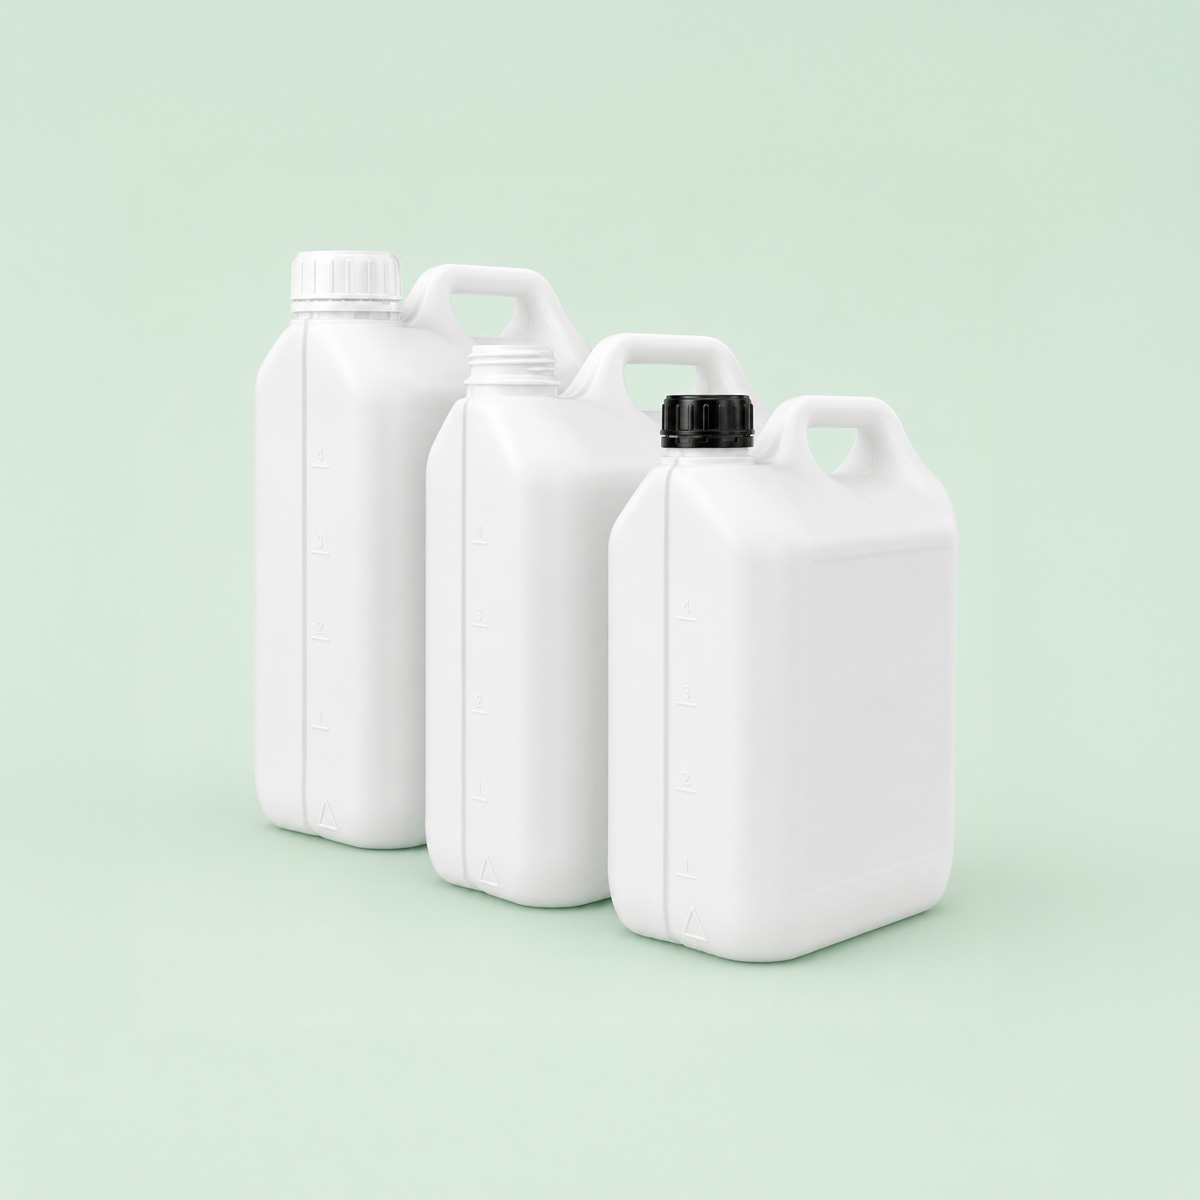
5L Jerrycan (Model 829)
Viewing window and graduated scale
Optimized weight
Integrated handle
Available with Ø38 and Ø50 neck finishes
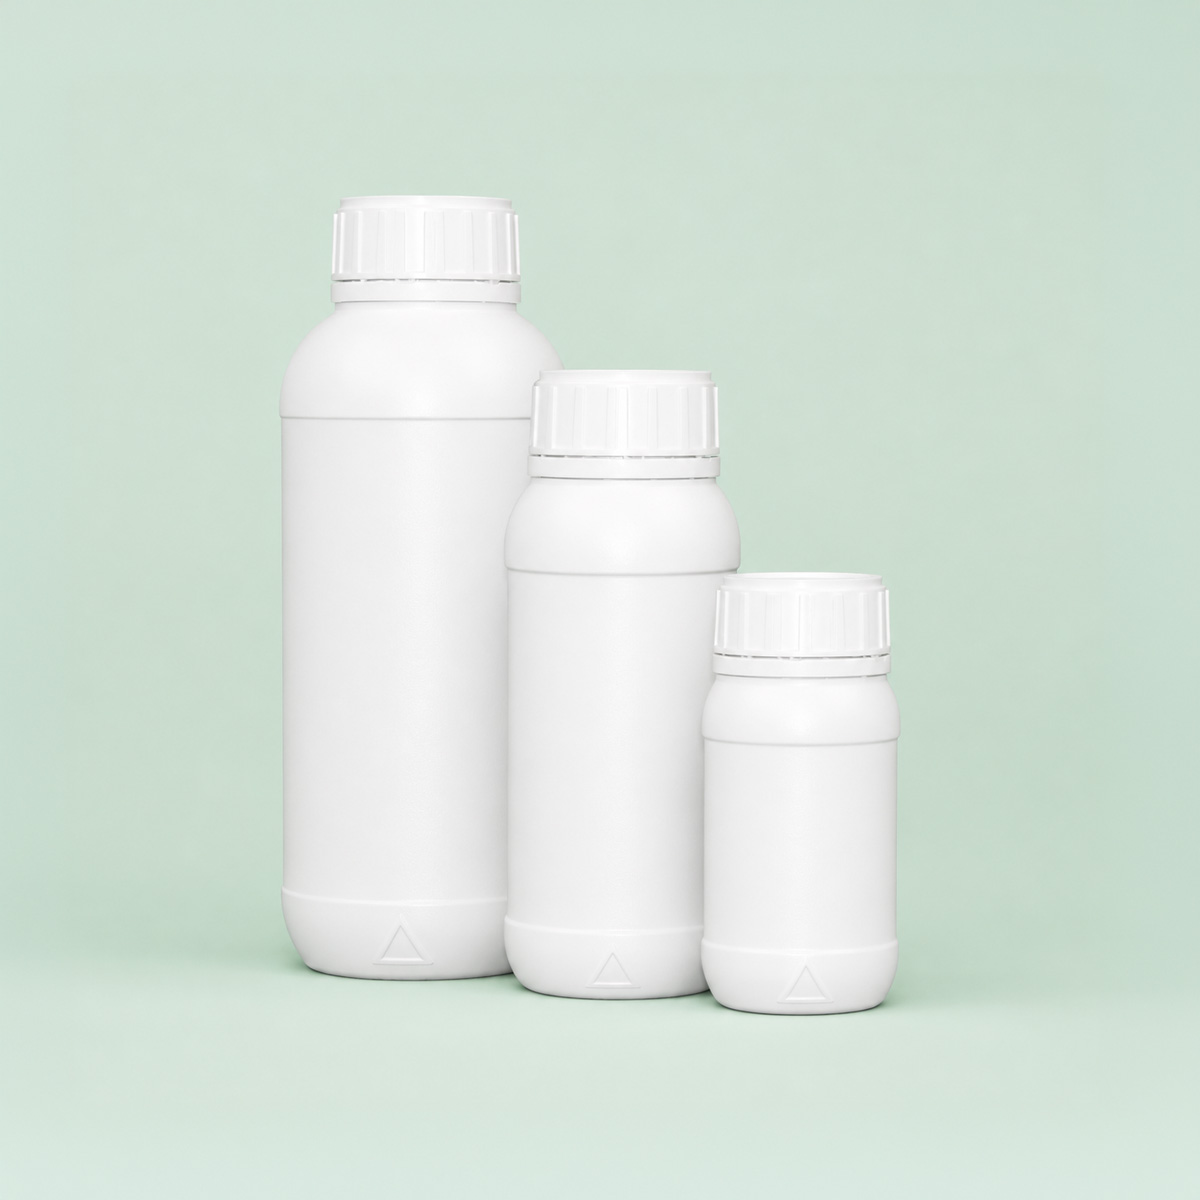
HDPE Bottles (Model 818)
Manufactured from HDPE
Available in 1L, 500ml, and 250ml capacities label recess panel
ADR Approved
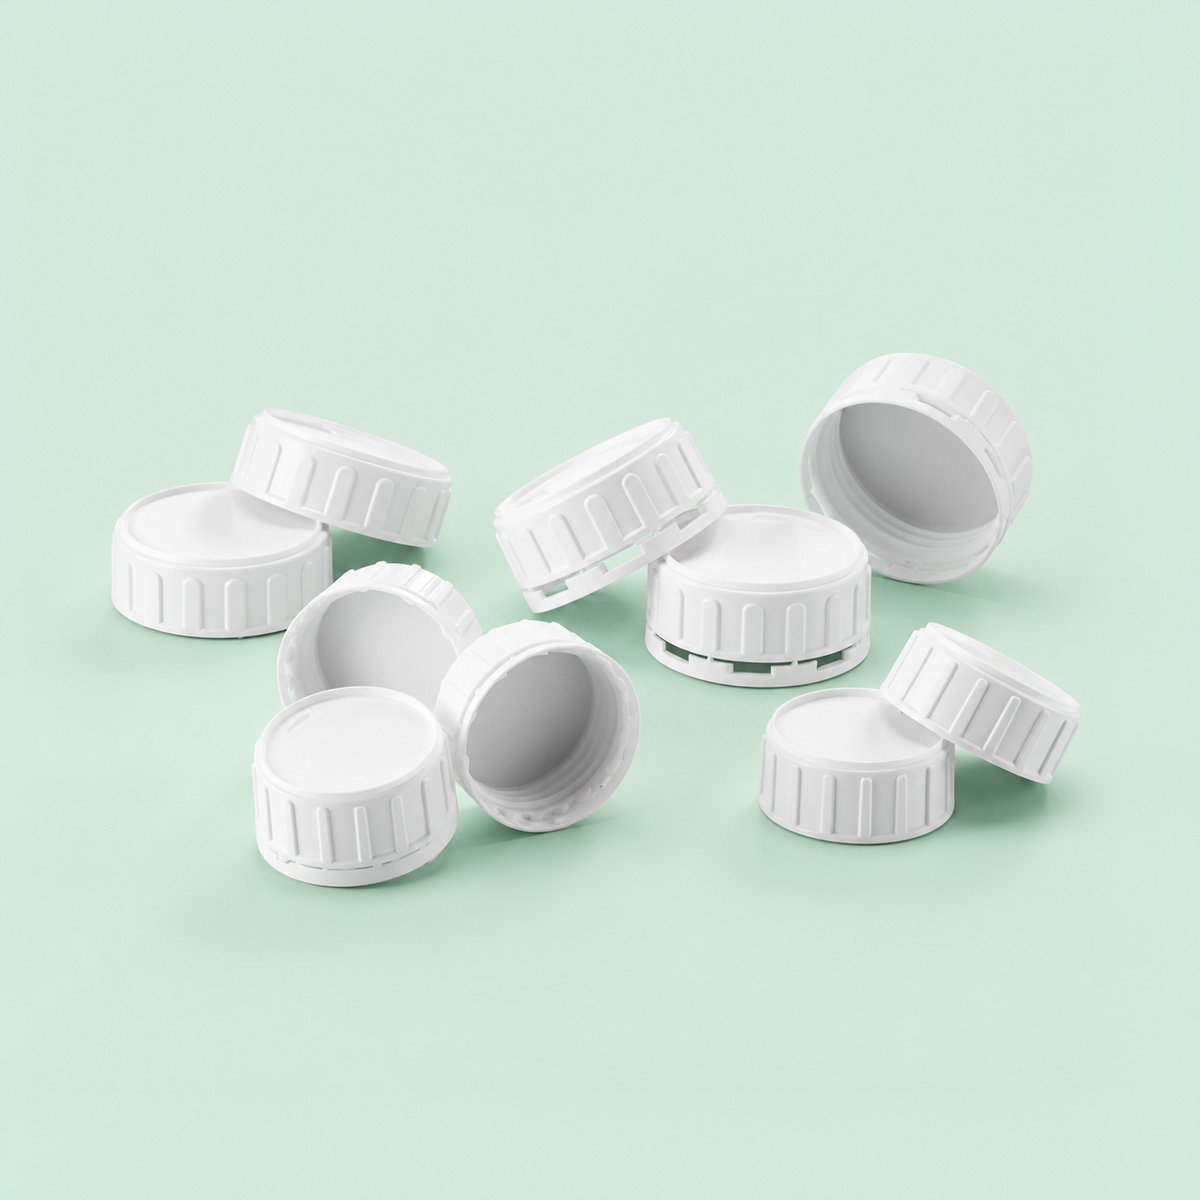
Caps
Induction Sealing liners
Foam liners
Degassing liners
Venting valve
What products and formats are best suited for your detergent formulations? Shall we talk?
Our chemical jerrycans protect formulations and help prevent product permeation.
Technical and sales support
We support you from the outset, helping you select the most suitable packaging solution for your product, manufacturing process and regulatory requirements.
Secure closure and pressure-control systems
Each component works together to prevent leaks, deformation, and issues caused by internal pressure build-up.
Regulatory compliance
We manufacture certified containers that comply with current regulations, guaranteeing safety and peace of mind at every stage.
Guaranteed industrial quality
We operate under strict quality controls to provide robust, consistent containers that meet the demands of industrial production
We are a certified company
Download our product catalogue
Access our technical catalogue of packaging solutions for detergents and water treatment applications.